

Oxygen absorbers are meant to help protect products from the bad effects of leftover oxygen that can sit inside sealed packaging. Still, how well they do the job depends on much more than the date that’s printed on the packet, or whatever format it comes in. Storage conditions, how much air they get exposed to, the absorber’s actual capacity and even the packaging quality all play a part. If manufacturers and exporters miss those details, it can cause product damage, lead to annoying quality complaints, and honestly create losses that could have been avoided.
So, how long do oxygen absorbers work? It depends on whether the absorbers are still sitting in their original, unopened packaging, or if they’ve already been placed inside a sealed product pack. Getting that difference clear helps a business plan buying cycles, manage inventory, and choose the right Oxygen Absorber for what their packaging needs are really like.
How Long Do Oxygen Absorbers Last?
Oxygen absorbers sort of come with two different “timelines” to keep track of, and people mix them up more often than you’d think.
Shelf life before use: This is the time period when an absorber is expected to still perform to its stated level while it’s stored in its original, unopened packaging, under recommended conditions.
Working life after use: This is the time period when the absorber removes oxygen from the sealed package. Also, the active reaction can wind down quite earlier than the packaged product hits the end of its own intended shelf life.
The oxygen absorber shelf life can vary a lot by product type, and by the manufacturer too. Some labels show a shelf life like 12, 24 , or 36 months. But those numbers aren’t universal, so it should be checked against the technical specification for the specific item you’re using. An oxygen absorber might stay suitable for months, especially if it’s stored properly.
Yet the moment you open the protective outer packaging, the sachets get exposed to air, and they start consuming the oxygen-absorption capacity they still have.
Quick Tip: Before buying, ask your supplier for the manufacturing date, the stated shelf life storage instructions, and batch identification details. a “one size fits all” statement about shelf life is not enough to approve every absorber model.
What Do Oxygen Absorbers Do?
Oxygen absorbers do what they sound like. They remove the oxygen that gets stuck inside a sealed package. A lot of everyday types use iron- based chemistry , and basically the iron reacts with oxygen. Then it turns into iron oxide, so there is less oxygen sitting in that pack. Regular air is around 20.9% oxygen.
Depending on the item, oxygen can be a problem for a few reasons, like oxidation and rancidity, plus color changes , loss of flavor, material degradation, or simply reduced product stability.
Oxygen absorbers may be used in suitable packaging applications involving:
- Products that are sensitive to oxidation
- Dry goods and products that need protection from oxygen exposure
Selected electronic components and other products where oxidation control is part of the packaging strategy. Certain pharmaceutical, nutraceutical and healthcare products, subject to application specific requirements.
Industrial materials where oxygen exposure may affect quality, or performance, in general. The correct solution depends on what exactly the product is that you are packing. A suitable absorber for one application may not be appropriate for another and that’s the part people forget.
Also, oxygen absorbers have a different purpose from desiccants. Desiccants, such as Silica gel, mostly control moisture, while oxygen absorbers reduce oxygen levels. Some packaging systems may need one, or both, depending on the hazards being managed
It’s important to know that removing oxygen doesn’t really replace other protective measures. You still need to account for product condition, packaging design, handling, storage, and the required safety controls too.

How Long Do Oxygen Absorbers Last in Sealed Packaging?
available. The time needed to reach the target oxygen level depends on the formulation, capacity, temperature, moisture conditions, and the package design too. Some absorbers may reach their goal in just hours, while others require longer time periods. The actual timing should be checked using the product specifications, and also application testing. Three factors deserve special attention.
1. Absorber capacity
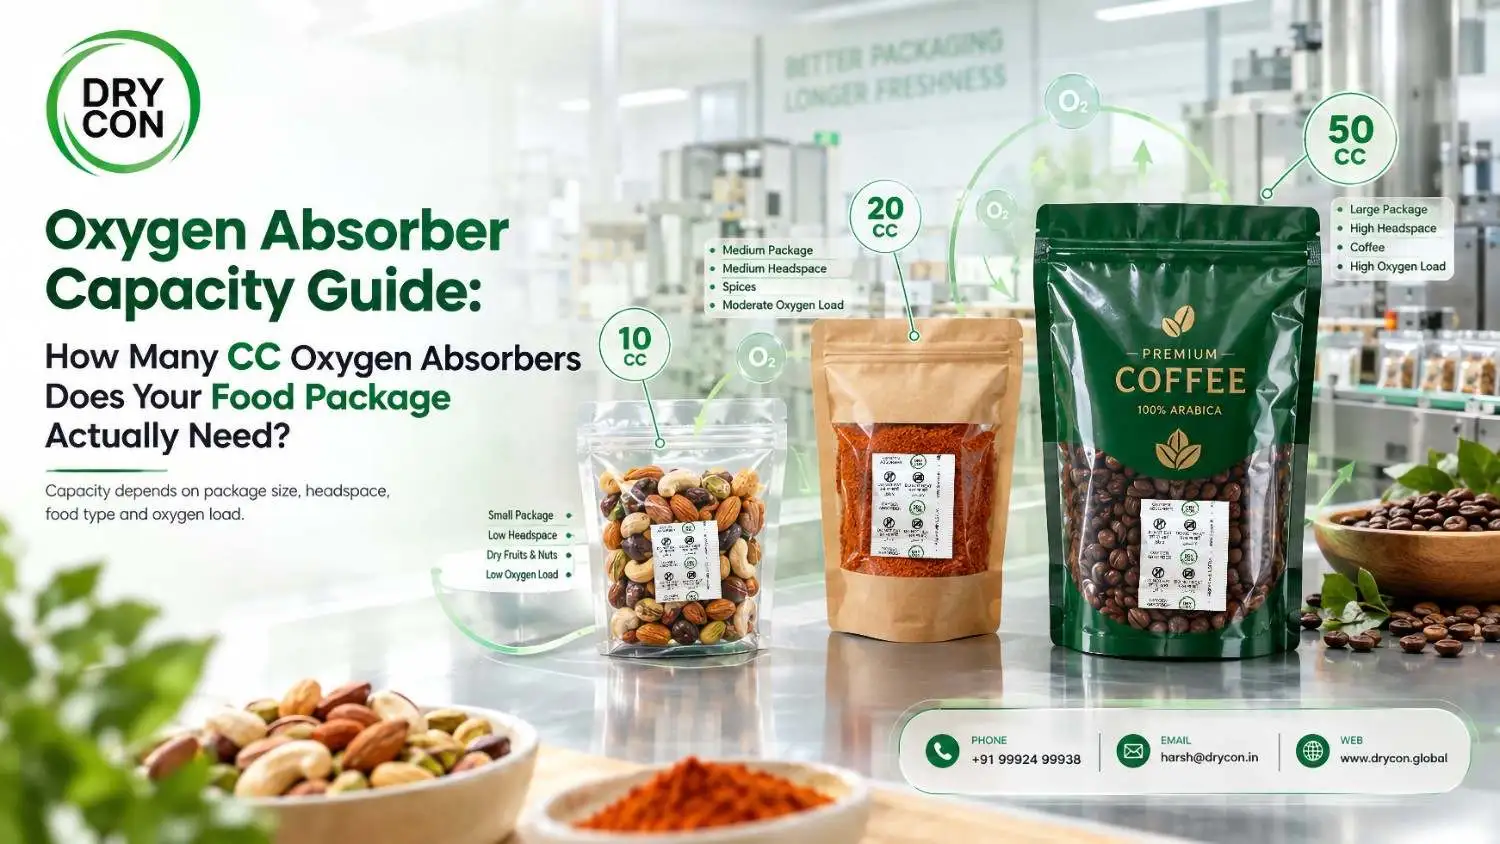
Oxygen absorption capacity is usually stated as cubic centimetres, (cc) of oxygen. The selected capacity really has to cover not just what gets trapped in there, inside the package, but also any oxygen that slowly comes in through the packaging, as time goes on.
If the absorber is too small, it can leave too much residual oxygen, sometimes more than you expect. If it’s too large, it may raise costs for no good reason, like there is no practical upside.
2. Packaging quality
Even a good absorber cannot keep oxygen levels low forever, if the package lets oxygen sneak in too quickly.
Film permeability, the seal quality, closures, small punctures, and any transport damage can all shift how well it performs. So absorber plus packaging… they need to work as one sort of system, not like separate pieces.
3. Product requirements
Different products have different oxygen sensitivity and they also need different kinds of oxygen absorber storage. So what protection you actually need can shift again with the package size, the expected shelf life, and the real distribution conditions , out in the world. To figure out how long oxygen absorbers will do their job inside a sealed package, manufacturers really should look at the entire packaging set up, not only the sachet by itself.
Also Read : How Many CC Oxygen Absorbers Does Your Food Package Actually Need?
How Long Do Oxygen Absorbers Last After Opening?
Opening the outer bag exposes the unused sachets to air. Their active material starts consuming oxygen, reducing the capacity available for use in the final package. Some manufacturers recommend using opened absorbers within 30 minutes to two hours. Other products may have different limits.
The correct period kind of depends on the absorber’s formulation, and basically the manufacturer’s instructions. So you follow that, not guess. For production teams, the practical idea is quite straightforward: open only the amount that can be used within the allowed time, otherwise you risk losing effectiveness.
How to Store Oxygen Absorbers Properly?
- Keep unused sachets in their original high barrier packaging.
- Reseal the outer bag right away after taking out the needed quantity.
- Use a validated airtight secondary container if the manufacturer says it is allowed.
- Write down when the outer bag gets opened, and then stick to the named usage limit.
- Keep the sachets away from heat, moisture, and pointless exposure to air.
- Shield the packets from punctures, crushing, and other physical damages.
Do not judge an absorber’s remaining capacity by appearance alone. A sachet can look normal without having enough capacity left to meet the application requirements.
What Affects Oxygen Absorber Shelf Life?
The oxygen absorber lifespan depends on how the product is made, packed, stored and handled before use.
| Factor | Possible Effect | What Buyers Should Check |
|---|---|---|
| Exposure to air | Uses up some absorption capacity before application | Opening limits and resealing instructions |
| Storage temperature | May affect product performance or packaging integrity | Approved temperature range |
| Humidity | Can influence activation in some formulations and may affect packaging integrity | Product-specific storage requirements |
| Outer packaging | Poor barrier protection may allow oxygen to reach unused sachets | Barrier properties and seal integrity |
| Sachet damage | May compromise the packet or its intended performance | Physical conditions and handling controls |
| Absorber capacity | Insufficient capacity may leave excessive residual oxygen | Capacity specifications and calculations |
| Final packaging | Oxygen ingress may reduce protection over time | Packaging barrier and seal testing |
| Stock rotation | Older stock may remain unused beyond its stated shelf life | Batch records and expiry tracking |
Do Oxygen Absorbers Expire?
Yes, oxygen absorbers do expire. They have a shelf life noted by the manufacturer and backed up by performance data, usually under specific storage conditions. So an oxygen absorber expiration date is basically the window where the item is expected to still meet its stated requirements and they don’t promise the same behavior beyond that.
That said, the date doesn’t always mean “instant failure” where they stop working the second the day changes or, like, every absorber immediately quits. But it also should not be assumed that performance is still reliable past the stated period, like, the moment it says it’s okay.
If that expired stock is on the table , the choice should be backed by the right technical evidence and also by your organization’s quality procedures, not just some quick look, even if it seems okay at first or it looks harmless. It is better to go by proper checks and clear proof rather than relying on guesswork only.
Also Read : Oxygen Absorber Cost vs Product Spoilage Cost: What Food Manufacturers Should Really Calculate
Can Expired Oxygen Absorbers Still Be Used?
In general, no, don’t approve expired absorbers just because they still look fine or because you see some reaction after they were exposed to air. A visible reaction doesn’t really prove that the full absorption capacity is still there. It only tells you that something happened, not how much active ability remains.
If someone is thinking about extending the usable period, then ask the supplier for an appropriate technical assessment and any relevant test results. The final call should follow your quality requirements and any applicable rules or regulations, not a “seems ok” kind of judgment.
Why does Oxygen Absorber Manufacturer Selection Matter?
Even if two oxygen absorbers claim the same capacity, they may not perform the same once you put them in a real packaging situation. Things like formulation, the sachet materials, manufacturing consistency, and quality checks can change the outcome more than people expect, even quite a bit.
A low purchase price can sound appealing, particularly when you’re ordering in bulk. But inconsistent performance can cause rejected goods, customer complaints, rework, and downstream losses that wipe out the small savings up front.
A dependable oxygen absorber manufacturer should be able to clearly explain the product specs, the quality checks used, storage requirements, and the intended applications—so you know what you’re actually getting.
Why does Laboratory Testing Matter?
Testing and quality check helps to confirm whether an absorber meets its stated capacity and performs as expected under defined conditions. It can also help identify problems with the sachet or the finished package , a bit sooner than later sometimes. Depending on the application, the relevant checks may include :
- Oxygen-absorption capacity testing
- Absorption-rate or residual-oxygen testing
- Sachet seal and integrity checks
- Evaluation of the finished packaging system
- Batch-specific quality records and traceability
Not every test is necessary for every application, so the test plan should kind of reflect the product, the packaging design, the expected oxygen absorber storage period and the risks that are being controlled, or at least trying to be controlled.
For products that have specific regulatory requirements, it is important to confirm the necessary documentation before approving a supplier. A general product statement doesn’t automatically establish compliance with every destination, or application requirement.
Also Read : ROI of Using Oxygen Absorbers in Food Packaging: A Practical Guide for Manufacturers and Exporters
An Industry Scenario: When the Lowest Price Is Not the Best Choice
A manufacturer preparing a large shipment for an overseas buyer. A new supplier offers oxygen absorbers at a lower price, with the same stated capacity as the product currently in use. The procurement team sees a chance to cut costs. Before approving the change though, the technical team checks the proposed product’s shelf life, oxygen absorber storage instructions, batch details and the supporting capacity information, just to be sure.
However the available documents do not really provide enough evidence to confirm that the new product will perform just as well inside the existing packaging. The team therefore requests samples and arranges suitable checks using the actual package design. The decision is not rejected because the new product is cheaper. It is held until the performance can be assessed.
This is a practical example of why supplier selection should involve both procurement and quality teams, not just one side maybe. A lower price can be worthwhile , but only when the product manages to meet the required specifications not just almost, you know.
A responsible oxygen absorber manufacturer should really explain what the product can do, and what evidence backs up its claims, plus where extra verification is still needed, for sure. Clear technical guidance helps buyers make decisions based on real performance rather than price only , and it should not feel vague.
Also Read : 15 Practical Benefits of Using Oxygen Absorbers in Food Packaging for Long Term Storage
How to Plan oxygen absorber Purchases and Storage?
Good stock planning reduces the risk of unused absorbers reaching their expiry date or losing usable capacity through sloppy handling and storage. Before placing a bulk order, consider these steps, step by step.
1. Estimate actual consumption. Calculate the number of sachets needed per production shift, day or month.
2. Match order quantities to usage. Avoid purchasing more stock than the business can reasonably use within the stated shelf life.
3. Account for lead times. Include manufacturing, transport, incoming inspection and production scheduling.
4. Check storage conditions. Confirm that the warehouse can maintain the conditions specified by the supplier.
5. Plan for opened bags. Give operators clear instructions on resealing, recording opening times and using the remaining sachets within the permitted period.
6. Track every batch. Maintain records of receipt dates, lot numbers and expiry dates.
7. Validate the finished package. Confirm the selected absorber and packaging provide the needed level of protection, not just at first.
For exporters too, also take into account transit time, destination requirements and the likely conditions during distribution. The product has to work for the whole trip, not only the initial packing.
Expert Buying Checklist for Oxygen Absorbers
Before signing off on an oxygen absorber supplier, take a careful look at these questions, just to be safe.
- What shelf life is stated for this exact model, no other one ?
- What temperature and humidity range are they specifying as required?
- How fast do the sachets need to be used after the pack gets opened, or is there a limit after exposure?
- What is the rated oxygen-absorption capacity, in the way they define it ?
- Is there supporting testing data available , such as reports or validated results?
- Can each supplied lot be identified and traced, with batch numbers that match records?
- Is the sachet actually suitable for the product itself and the real packaging environment?
- Does the packaging give an adequate oxygen barrier, not just “good enough”, but documented?
- Can the supplier provide the technical documents you need for your specific application?
- Can they help with sample evaluation, plus ongoing supply planning when production ramps up?
A solid supplier should answer these items plainly, or they should point out which areas still need extra verification, rather than leaving you guessing.
For procurement teams, resolving these questions before you issue the purchase order can cut down uncertainty during production, and also during the quality approval steps.
Also Read : Oxygen Absorber Manufacturer Evaluation Guide for Food Packaging Buyers